Clear PVC Cosmetic Bags: Materials, Compliance and Sourcing Guide
Executive Summary
Can a clear PVC cosmetic bag hold liquids, pass a chemical compliance review, and still read as genuinely see-through at a security checkpoint? Yes, but only when the specification names the film gauge in millimetres and grams per square metre, states the plasticiser system, and identifies the seam joining method rather than relying on the words clear PVC. Buyers writing a transparent makeup bag specification work to a minimum order quantity of 500 pieces per style and colourway, sampling in 6-10 working days, bulk production of 35-50 days after sample approval, and inspection at AQL 2.5 under ISO 2859-1.
The decisions that actually determine satisfaction are not aesthetic. Unsupported film versus PVC-coated polyester base fabric changes tear behaviour and weld behaviour. Gauge changes stiffness on a cubic relationship, so a 0.30 mm film is roughly three times stiffer than a 0.20 mm film of the same compound. Radio-frequency welding produces a liquid-tight seam on PVC and TPU but not on polyethylene-based films, which need heat sealing instead. Print coverage, meanwhile, directly consumes the see-through property the product exists to deliver.
Chemical compliance and long-term appearance close the picture. Certain phthalates are restricted under EU REACH, and cosmetic contents such as fragrance oil, alcohol and acetone attack plasticised film. Clouding, cold cracking and yellowing are all traceable to formulation choices made at the film stage, which is why the laboratory evidence requested before approval matters more than the sample in the post.
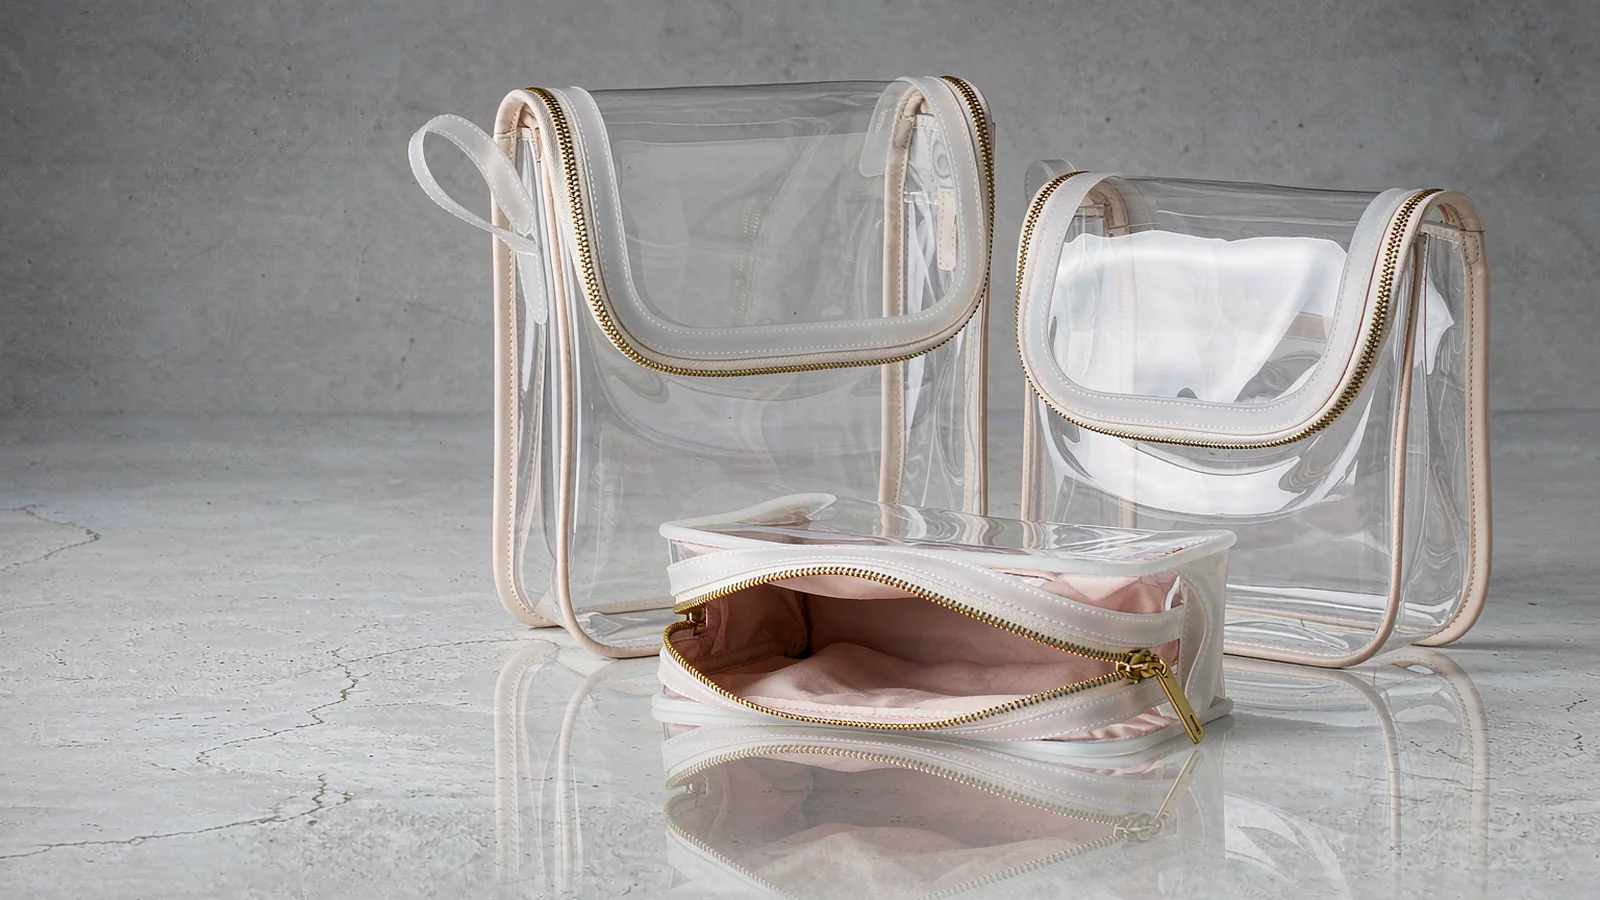
What Clear Means When You Specify a Transparent Cosmetic Bag
Clear is not a material. It is a cluster of measurable optical and mechanical properties that two suppliers can deliver at very different levels while both honestly describing the product as transparent construction. Buyers who write the single word clear into a specification routinely receive goods that are technically transparent and commercially wrong: too stiff, too hazy, too smelly, or prone to cracking in a cold warehouse. The remedy is to break clear into named attributes and write each one as a line item with a number and a test method attached: light transmission, haze, film gauge, and seam liquid hold-out.
Three polymer families dominate transparent bag construction. Flexible PVC is polyvinyl chloride resin compounded with a plasticiser, a heat stabiliser and lubricants; it is the lowest-cost route to a glass-clear film and it welds beautifully under radio-frequency energy because the polymer is polar. TPU, thermoplastic polyurethane, is an elastomer that needs no plasticiser at all and gives better low-temperature flex, better abrasion resistance and better oil resistance, at a material cost that is typically several times higher. EVA and PEVA, ethylene-vinyl acetate and its polyethylene-modified cousin, are cheaper and softer but read as translucent rather than clear, with a frosted or milky cast that many buyers find unacceptable in a cosmetic pouch.
| Attribute | Flexible PVC film | TPU film | EVA / PEVA film | Moulded rigid PET |
|---|---|---|---|---|
| Typical gauge used in bags | 0.15-0.50 mm | 0.10-0.30 mm | 0.12-0.40 mm | 0.60-1.20 mm |
| Optical character | Glass clear, low haze when fresh | Glass clear, very low haze | Translucent to frosted | Clear but rigid and brittle if thin |
| Hand and drape | Stiffens sharply with gauge | Soft, elastic, good drape | Soft, slightly rubbery | No drape, holds a moulded shape |
| Low-temperature behaviour | Depends entirely on plasticiser choice | Stays flexible well below freezing | Good, but weak at low gauge | Brittle below room temperature in thin sections |
| Plasticiser content | High, typically 25-40 percent of compound | None | None | None |
| RF / high-frequency welding | Excellent | Good to excellent | Poor, non-polar | Not applicable |
| Heat sealing | Possible but risks scorching | Possible with correct dwell | Excellent | Not applicable |
| Odour tendency | Noticeable when fresh | Low | Low to moderate | Very low |
| Relative material cost band | Lowest of the flexible films | Highest | Low to moderate | Moderate, plus tooling cost |
| Typical end use | Flat pouches, hanging toiletry kits, venue-style totes | Premium pouches, cold-climate programmes | Light pouches, wet bags, low-price lines | Structured vanity cases and rigid organisers |
The chemistry explains the behaviour. In flexible PVC the plasticiser is a liquid held physically, not chemically, inside the polymer. That liquid is what makes the film soft, and it is also the source of most of the failure modes: it migrates to the surface and causes haze, it evaporates and causes odour, it is extracted by oils and solvents in cosmetic products, and it can be a restricted substance under chemical law. TPU avoids all of that because its softness is built into the polymer chain, which is precisely why it costs more.
- Unsupported calendered film — a single homogeneous sheet of flexible PVC, no textile inside; welds cleanly, tears once nicked, used for flat pouches and lightweight totes.
- Knife-coated or transfer-coated fabric — PVC compound applied onto a polyester or nylon woven scrim; the scrim carries load and stops tear propagation, used for larger bags and any style with a handle.
- Laminated film-to-knit — a clear film bonded to a light knit for a softer hand and less crease whitening at folds.
- Coated-fabric seam sealing — the coated construction can be welded on the coating side, but cut edges expose the scrim and need binding or taping.
- Unsupported film with printed border — a common compromise in security-screening styles, where the central panel is left unprinted.
Choosing between unsupported film and PVC-coated base fabric is a structural decision, not a cost decision alone. Unsupported film has no textile reinforcement, so a 2 mm nick at the zipper end can propagate across the panel under load; its advantage is a perfectly clean weld and a truly uninterrupted window. Coated fabric puts a woven polyester scrim inside the sheet, which arrests tears and lets the bag carry handles and heavier contents, at the price of slightly lower light transmission, visible weave texture, and cut edges that must be bound because the exposed scrim wicks water. Bags above roughly 30 cm in any dimension generally justify coated construction.
Because coated fabrics carry a textile component, their mechanical behaviour is characterised by a different family of test methods than plain films, and the standard most often cited for this purpose is ASTM D751, the test method collection for coated fabrics covering tensile, tear, coating adhesion and low-temperature bend behaviour. Referencing that framework in a specification tells a laboratory exactly which measurements to run. Textile components inside a coated construction also carry their own obligations: a recycled-content claim on the polyester scrim should be supported by chain-of-custody documentation under the Global Recycled Standard, and any dyed scrim should meet the colour-fastness expectations set out in the ISO 105 series.
A specification line that reads clear PVC invites interpretation. A line that reads 0.30 mm unsupported flexible PVC film, 390 g per square metre, haze below 8 percent measured on a haze meter, non-phthalate plasticiser system, does not. Writing optical and dimensional numbers into the first draft of a specification typically removes one full sampling round from the calendar.
Gauge, Thickness and Hand: Reading a Film Specification Correctly
Film thickness is where most transparent bag specifications quietly fail, because the industry uses at least four overlapping naming systems and suppliers switch between them mid-conversation. North American vinyl trade habit expresses thickness in mil, where one mil is one thousandth of an inch. British and some Asian film conventions use a gauge number where 100 gauge equals one mil. Continental and technical specifications use millimetres or microns. Purchasing departments often ask for grams per square metre because it appears on the invoice. All four describe the same sheet and none is interchangeable without a conversion.
In US vinyl usage a 6-gauge film means six mil, about 0.15 mm. Under the older British film convention a 600-gauge film means six mil. A supplier quoting 8 gauge and a buyer hearing 0.8 mm are describing sheets that differ by a factor of four. Always restate thickness in millimetres and in grams per square metre in the written specification and require the supplier quotation to repeat those two figures back.
| Nominal gauge (mil) | Millimetres | Microns | Approx. g/m² at 1.30 density | What buyers typically use it for |
|---|---|---|---|---|
| 4 mil | 0.10 mm | 100 µm | 130 g/m² | Dust covers, inner liners, promotional flat sleeves |
| 6 mil | 0.15 mm | 150 µm | 195 g/m² | Light flat pouches, single-panel cosmetic sleeves |
| 8 mil | 0.20 mm | 200 µm | 260 g/m² | Standard clear cosmetic pouch body, pencil-case formats |
| 10 mil | 0.25 mm | 254 µm | 330 g/m² | Mid-weight pouch, hanging toiletry panels, wet bags |
| 12 mil | 0.30 mm | 305 µm | 396 g/m² | Structured pouches, security-screening style totes |
| 16 mil | 0.41 mm | 406 µm | 528 g/m² | Heavy-duty toiletry kits, vanity case bodies |
| 20 mil | 0.51 mm | 508 µm | 660 g/m² | Stiff panels, base inserts, semi-rigid organisers |
Grams per square metre cannot be derived from thickness alone, because each polymer has a different density. The conversion is straightforward: grams per square metre equals thickness in microns multiplied by density in grams per cubic centimetre. Flexible PVC compound sits around 1.25 to 1.35, TPU around 1.18 to 1.22, and EVA around 0.93 to 0.96. A 250 micron sheet therefore weighs about 325 grams per square metre in PVC, about 300 in TPU, and only about 238 in EVA, so two quotations promising the same thickness can differ by more than 25 percent in delivered weight purely because of density.
Stiffness is the property buyers actually feel, and it does not scale linearly with thickness. Bending stiffness rises with the cube of thickness, so moving from 0.20 mm to 0.30 mm makes the same compound roughly three times stiffer, not fifty percent stiffer. This is why a transparent pouch that feels pleasingly soft in a 0.20 mm sample becomes a rigid box at 0.30 mm, and why a buyer who wants structure is often better served by staying thin and adding a coated scrim or a bound frame. It also explains the most common sampling surprise in this category: the approved sample was floppy and the bulk order arrived board-stiff.
- Flat zip pouch up to 24 cm wide — 0.15 to 0.20 mm unsupported film gives a soft, packable hand.
- Hanging toiletry kit with multiple compartments — 0.20 to 0.25 mm, or 0.18 mm coated onto a light scrim for tear resistance at the hook.
- Structured vanity or train case — 0.30 to 0.45 mm, usually coated fabric with binding on all cut edges.
- Security-screening or venue-style tote — gauge matched to the venue's own published envelope, mid-range so the bag holds shape when empty.
- Promotional or gift-with-purchase pouch — 0.12 to 0.18 mm, where unit cost dominates and service life is short.
Thickness also drives the welding process. Radio-frequency welding heats the material volumetrically, so a thicker film requires more energy and a longer dwell, and the electrode must apply enough pressure to avoid thinning the weld line. In practice a weld on 0.40 mm film shows a visible bead and a reduction in cross-section at the seam unless die pressure and cycle time are tuned together, and an undertuned weld on heavy film is the most common cause of a seam that passes a visual check and then weeps under a 24-hour water test. Buyers should ask which weld cycle parameters were used and whether they are recorded per batch.
Finally, thickness has a tolerance. Calendered PVC film typically varies by several percent across and along the roll, and that variation is invisible to the eye but material to both weight and weld consistency. A specification should state a target thickness, a tolerance band and the measurement method, and should require the supplier to report measured values at several points across a panel. Where coated fabric is used, coating thickness and total thickness are separate measurements and both matter, and ASTM D751 is the conventional framework describing how those measurements and the associated coating adhesion checks are performed.
Seams That Hold Liquid: RF Welding, Heat Sealing and Stitched-and-Taped Construction
A transparent toiletry bag is judged on whether it holds a leaking bottle of shampoo, and that judgement is made at the seam. There are four leak paths in any sewn or welded pouch: the perimeter seam itself, the needle holes if it was sewn, the zipper installation, and the corner radii where two weld lines meet. Of these, the perimeter seam gets the most attention and the zipper installation causes the most field complaints, because a zipper tape is a different material from the body film and must be joined to it without leaving a channel at the stops.
Radio-frequency welding, also called high-frequency or dielectric welding, works by placing the film between electrodes and applying an alternating electric field, commonly at 27.12 MHz. Polar molecules in the material attempt to rotate with the field and generate heat internally, so the film melts from within and fuses under pressure. PVC welds extremely well by this route because it is strongly polar. TPU welds well. Polyethylene, polypropylene and EVA or PEVA do not, because they are non-polar and generate little internal heat, so those materials must be joined by conductive heat sealing from a heated bar, wedge or impulse element instead. Specifying a welded seam on a PEVA bag without naming heat sealing produces a weak, partially fused joint.
| Joining method | Mechanism and materials it suits | Liquid hold-out | Tooling and cost implications | Best application |
|---|---|---|---|---|
| RF / high-frequency welding | Dielectric heating of polar polymers; PVC and TPU | Fully liquid-tight when tuned | Copper or brass die per shape, moderate tooling cost, fast cycle | Perimeter seams, compartment dividers, zipper insertion on PVC |
| Hot-wedge heat sealing | Conducted heat from a travelling wedge; PE, PP, EVA, PEVA | Liquid-tight, narrower process window | Low tooling cost, slower on curves | Long straight seams on polyethylene-based films |
| Hot-bar or impulse sealing | Heated bar pressed for a set dwell; thin PE and EVA films | Liquid-tight on flat runs, weak at corners | Lowest tooling cost, manual or semi-automatic | Simple flat pouches, low-volume runs |
| Stitched and taped | Needle seam then PVC tape welded over it | Liquid-tight until tape edge lifts | No weld die needed, extra labour and material step | Structured bags, handle attachment, heavy loads |
| Stitched and bound | Needle seam covered by a folded binding, not sealed | Not liquid-tight; leak path through needle holes | Lowest cost, most conventional appearance | Cosmetic bags sold as organisers, never as wet bags |
| Ultrasonic welding | Frictional heating at a horn; some TPU and synthetics | Variable on films, better on thicker sections | Horn tooling per profile, higher capital cost | Specialist applications, tabs and small fixtures |
Seam quality is expressed as weld efficiency, the strength of the joint as a percentage of the strength of the parent film around it. A well-tuned RF weld on PVC can approach the parent material, meaning the film tears before the seam separates, and buyers can request that relationship be demonstrated rather than asserted. The relevant measurements are a shear test pulling the seam in line and a peel test separating it, with ASTM D751 as the conventional framework for tensile, tear and adhesion measurement on coated fabrics. Buyers should also ask for a hold-out test result rather than accepting a visual inspection of the weld bead.
Zippers deserve their own specification line. A clear pouch normally takes a coil zipper whose tape has been formulated or coated to weld to the body, because a polyester tape will not fuse under RF energy unless it carries a weldable coating. The end stops are the weak point: if the weld does not terminate cleanly at the stop, a capillary channel remains and the bag drips when laid on its side. Terminology for zipper components, including tape, chain, slider and stop, is standardised in ASTM D2053, and using those terms in a specification removes a surprising amount of ambiguity when quotations are compared across suppliers.
- Corner radius of at least 6 mm — sharp corners concentrate stress and thin the weld where two seams meet.
- Perimeter weld width of 5 to 10 mm — narrower welds look cleaner but leave less tolerance for cycle variation.
- Weld terminating flush with the zipper end stop — the most reliable way to close the capillary leak path.
- Bound or taped cut edges on coated constructions — an exposed scrim wicks liquid into the seam.
- Recorded weld cycle parameters — energy, dwell and pressure logged per batch makes a field failure diagnosable.
- A defined leak test at sampling and at inspection — fill, lay flat on absorbent paper, and hold for a stated period.
Stitched-and-taped construction remains the right answer for some products despite its extra step. When a transparent bag must carry a strap, a hanging hook or a heavy glass bottle, the load path runs through a seam that no film weld should carry alone, and a needle seam reinforced with an RF-welded PVC tape distributes that load into the scrim of a coated fabric. The failure mode to watch is tape edge lift after exposure to cosmetic oils. Buyers ordering this construction should specify tape width, weld width on each side, and an adhesion check after oil exposure.
On the commercial side, seam method affects tooling and the sampling calendar. A welded construction needs a die cut to the panel profile, which adds a tooling step and pushes a first sample toward the longer end of the 6-10 working day window, or into the 12-15 working day band for multi-panel constructions. The die is shape-specific, so a brand planning three sizes should expect three dies or a modular strategy, while heat-sealed polyethylene avoids the die entirely.
Printing and Branding on a Transparent Surface Without Defeating the Purpose
Branding a clear bag contains a paradox: the product exists to be looked through and the brand exists to be looked at. Every square centimetre of opaque ink is a square centimetre of the window permanently closed, and in security-screening contexts that trade-off decides whether the bag functions or is turned away. Resolving it means treating print as a placed element with a defined coverage budget rather than a logo dropped onto a panel.
Print adhesion on plasticised PVC is its own technical problem. Solvent-based PVC inks work by slightly swelling the film surface so the resin keys into it, which is effective but requires the ink to be compatible with the plasticiser in that specific film. When it is not, the plasticiser migrates into the ink film over weeks, producing a tacky surface, colour bleed, and blocking where stacked bags stick together in the carton. Energy-cured digital inks sit on the surface instead and need corona or primer pre-treatment on flexible PVC. Either way, a printed clear bag should be aged before approval rather than judged on the day it comes off the line.
| Branding method | How it bonds to the film | Effect on see-through area | Durability consideration | Order implication |
|---|---|---|---|---|
| Screen print, solvent PVC ink | Swells and keys into the film surface | Fully opaque in the printed area | Excellent if plasticiser-compatible; tacks up if not | Screen per colour, economical at volume |
| Heat transfer print | Heat and pressure set a printed layer | Fully opaque in the printed area | Can lift at folds and corners | No screens, good for multi-colour logos |
| UV-cured digital print | Cures on the surface, needs pre-treatment | Fully opaque, fine detail possible | Edge chipping at creases; check adhesion after ageing | No plates, viable for short runs and personalisation |
| Hot foil stamping | Heat and pressure transfer a metallic layer | Fully opaque, small areas only | Heat can distort thin film; test dwell carefully | Die per logo, premium appearance |
| Woven label in binding or seam | Sewn into the construction | Zero central-window loss, edge only | Outlasts any print on film | Adds a sewing operation and a label minimum |
| Metal or moulded logo plate | Riveted or pressed onto a panel or puller | Minimal, a few square centimetres | Very durable; adds weight and a hard point | Tooling for a custom plate, higher unit cost |
| Frosted or etched effect | Matte lacquer or UV varnish diffuses light | Diffuses but still transmits light | Scratch-sensitive; fingerprints show | No colour limitation, subtle branding |
The practical rule is to place branding in a border zone rather than across the field of the panel. A printed band across the top header, down one vertical edge, or around a bound frame gives the brand a readable mark while leaving the central window intact, and it also solves a production problem: a print registered to a border is far easier to keep consistent than one floating in the middle of a flexible panel. As an illustrative planning guide rather than a rule, many programmes keep opaque coverage below roughly a quarter of each face, and any programme intended for security-screening use should confirm the permitted coverage in the venue's own policy before artwork is finalised.
- Printed header band — maximum brand presence with the window untouched; the default choice for screening-oriented styles.
- Printed border frame — reads as deliberate design and hides minor film haze around the edges.
- Corner logo block — small footprint, easy registration, still leaves the centre clear.
- Frosted logo patch — brand visible, light still transmitted, useful when the venue requires transparency but the brand wants presence.
- Woven label at the binding — zero loss of viewing area, the safest option for compliance-sensitive programmes.
- Full-panel print — maximum impact, defeats the see-through function; reserve it for gift pouches with no screening purpose.
Several non-print options deserve consideration before artwork is commissioned. A moulded metal plate on the zip puller carries a logo at almost no cost to transparency and reads as a quality signal. An embossed film logo catches light without adding ink, a coloured yarn in the binding carries brand colour, and a removable printed insert card in a back pocket suits multi-channel labelling.
Tinted film is a separate decision from printing. A transparent bag can be produced in a clear, a lightly tinted or a saturated coloured film, and each step up in tint reduces transmitted light and makes contents harder to identify. Light tints are popular because they hide the discolouration of contents over time. Dense tints and opaque colours should be treated as a different product entirely: they do not deliver the see-through function, and calling them clear in a listing risks a complaint and, in a screening context, a refused entry. Where a tinted film is chosen, the buyer should state a target transmission and treat it as an inspected attribute rather than a shade match.
There is also a compliance reason to control print inputs. Pigments and inks can be in scope for restricted-substance screening, and the finished clear bag is usually assessed as an article with a surface coating. Buyers selling into the EU and the US commonly require finished-goods screening against restricted-substance lists and, for children's products, against toy-safety migration limits. Specifying the ink system in the same document as the film means the laboratory receives a complete bill of materials rather than a film sample with unknown print chemistry on it. Print chemistry can be assessed against OEKO-TEX Standard 100, and restricted substances in articles are administered in the EU through the REACH framework published by the European Chemicals Agency.
Clarity Retention, Clouding, Cold Crack, Odour and Yellowing
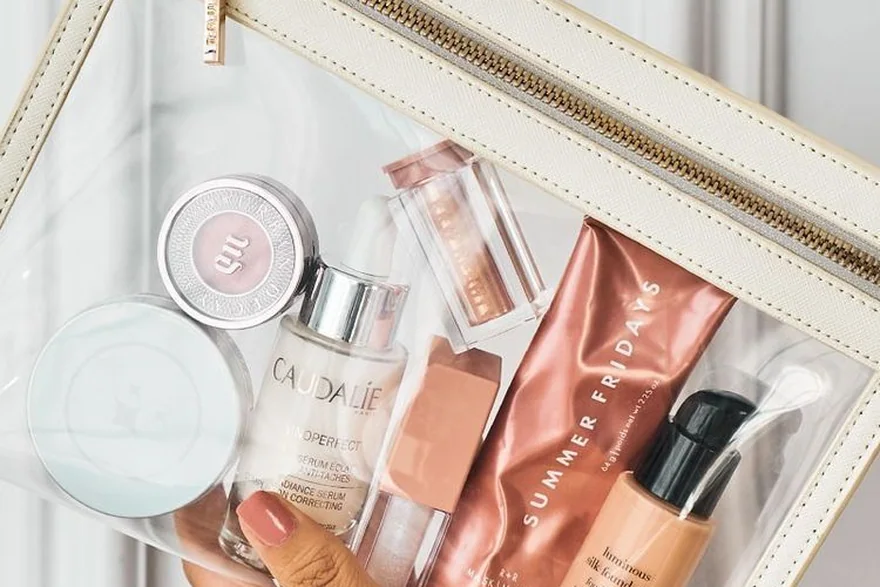
Every transparent bag changes after it leaves the line. How fast, and by how much, is largely determined by formulation choices made before the buyer ever sees a sample. Clarity retention has two measurable halves: light transmission, the proportion of light passing through, and haze, the proportion scattered. A film can have high transmission and high haze, which is exactly what frosted PEVA looks like, so a specification that asks only for clear will accept it. Buyers who care about optics should state a haze target and require it to be measured with a haze meter.
| Failure mode | Primary cause | Where it appears first | Lever available to the buyer |
|---|---|---|---|
| Surface haze or bloom | Plasticiser migrating to the surface | Across flat panels, worst where two faces touch | Specify a higher-molecular-weight or polymeric plasticiser system |
| Crease whitening | Stress-induced crazing at a fold | Along fold lines and packed corners | Reduce gauge or switch to TPU, which recovers better |
| Blocking marks | Film adhering to itself under heat and pressure in storage | Broad cloudy patches on stacked panels | Require anti-block additive and embossed film, and cool before cartoning |
| Inter-layer fogging | Moisture trapped between film and liner or between stacked panels | Random patches after a humid shipment | Specify drying, breathable packing and a desiccant in the carton |
| Cold cracking | Plasticiser losing solvating power at low temperature | Fold lines and zipper ends in winter | Specify a low-temperature plasticiser and require a low-temperature bend test |
| Yellowing | Thermal dehydrochlorination or UV oxidation | Sun-facing panels and heat-exposed areas | Specify a stabiliser package with UV absorber and avoid aromatic grades |
| Persistent odour | Residual solvent, monomer or volatile plasticiser | On opening the carton and the bag | Specify low-odour grades, aeration before packing, and a graded odour limit |
| Tackiness after use | Plasticiser extracted by cosmetic oils or solvents | Interior floor of the bag, under bottles | Switch to TPU or a higher-molecular-weight plasticiser; test with the actual product formulation |
Cold crack is the failure that surprises buyers most, because it appears months after approval and only in one season. Flexible PVC stiffens as temperature falls, and the temperature at which it turns brittle is governed by the plasticiser, not the resin. General-purpose plasticisers give moderate low-temperature performance, while adipate and sebacate types and certain cycloaliphatic non-phthalate types are chosen specifically for cold flexibility. A bag shipped to a market with unheated warehousing needs that choice made explicitly, expressed as a low-temperature bend test on the coated fabric or film from the ASTM D751 collection, with the conditioning temperature, fold geometry and acceptance criterion stated rather than a generic request for cold resistance.
Yellowing has two distinct mechanisms and they are not fixed by the same additive. In PVC, heat or UV exposure can strip hydrogen chloride from the polymer chain, creating conjugated double bonds that absorb visible light and turn the film yellow, then amber, then brown; an adequate heat stabiliser package, typically calcium-zinc based in modern non-toxic compounds with a co-stabiliser, is the defence. In TPU, yellowing is usually photo-oxidation of the aromatic segments and is addressed by choosing an aliphatic grade or adding UV absorbers and hindered amine light stabilisers. There is also a storage mechanism in which nitrogen oxides react with phenolic antioxidants in packaging, producing discoloration that transfers to the bag, which is why carton and polybag choice belongs in the specification. Colour-fastness behaviour of any dyed textile component alongside the film is assessed under the ISO 105 series, and textile-specific ageing and storage tests are catalogued in the AATCC test methods catalogue.
Odour is the complaint that generates the most retail returns in this category, and it is almost entirely a specification problem. The smell buyers associate with a new shower curtain comes from volatile compounds leaving the film: residual solvent from printing, residual monomer, and the more volatile fraction of the plasticiser. It fades with time, but the buyer cannot rely on the customer waiting. The practical controls are low-odour plasticiser and ink systems, a defined aeration period between production and packing, no airtight packing while the bag is still warm, and a graded odour acceptance limit assessed by a trained panel under stated conditioning.
- Plasticiser system — the single largest influence on odour, cold flex, extraction resistance and restricted-substance status.
- Stabiliser package — governs yellowing under heat and UV; calcium-zinc systems dominate non-restricted compounds.
- UV package — absorbers and light stabilisers extend outdoor and window-display life for aromatic TPU.
- Film gauge and strain — thicker film and tighter folds both accelerate crease whitening.
- Storage and packing — cool before cartoning, use breathable packing, avoid phenolic-antioxidant-rich cartons, add desiccant for humid routes.
- Contact chemistry — specify the actual cosmetic formulations the bag will meet, and test against them rather than against water.
Chemical compatibility with contents is worth testing explicitly, because cosmetic products are aggressive solvents. Fragrance and essential oils, high-alcohol toners, acetone-based nail polish remover, and some sunscreen filters extract plasticiser from PVC and can soften, haze or craze the interior within a short period. TPU resists oils and abrasion far better and is the usual upgrade path for oil-based product lines, while polyethylene-based films resist many solvents but bring their own clarity and stiffness compromises. A compatibility test should run the brand's actual formulation on the interior surface at a stated temperature and duration, with the acceptance criterion written before the test rather than negotiated afterwards.
Security Screening, Chemical Compliance and the Written Specification
Transparent bags are bought for screening contexts because they let a screener see contents without opening the bag, which shortens queues and reduces physical searches. The most widely recognised driver of demand for a small clear toiletry bag is the airline carry-on liquids rule, under which travellers consolidate containers into a single transparent bag; the US Transportation Security Administration publishes and updates its liquids rule, so the current published version is the only reliable reference. Beyond aviation, event venues, arenas and festivals apply their own bag policies, and that is where buyers must be careful.
There is no universal clear-bag size. Stadium, arena and festival entry rules are set by each operator, differ between venues that look identical, and are revised between seasons, so a dimension that was accepted last year may not be accepted now. A buyer supplying bags for venue entry must verify the requirement against the specific venue's current published policy, in writing, before artwork and tooling are committed, and should treat any stated dimension as that venue's rule, not an industry standard. Printing the words stadium approved on a bag is a claim the brand must substantiate against each venue it names.
Chemical compliance is the other half of the risk picture, and it starts with the plasticiser. In the EU, several ortho-phthalates including DEHP, DBP, BBP and DIBP are restricted in articles above a low percentage threshold of the plasticised material, which is why a clear PVC cosmetic bag sold into Europe is normally specified as non-phthalate. The restriction framework and the candidate list of substances of very high concern are administered under REACH, and the European Chemicals Agency publishes the regulation and annexes. In the United States, the Consumer Product Safety Improvement Act sets phthalate limits for children's products and child care articles, and California maintains its own listed-substance regime, so a programme sold into both markets needs the destination list stated on the specification.
Non-phthalate alternatives each carry a trade-off, which is why the choice belongs to the buyer rather than to whoever compounds the film. DOTP, also written DEHT, is the closest general-purpose drop-in, with good but not exceptional cold behaviour. DINCH is a cycloaliphatic ester chosen for low migration, with moderate cold performance. ATBC is a citrate ester with good compatibility but higher volatility and cost. Polymeric adipates deliver excellent cold flex and permanence at a higher price. Epoxidised soybean oil functions mainly as a co-stabiliser rather than a primary plasticiser. The correct answer depends on the sales market, the cold-chain reality and the contents chemistry, and it should be written into the specification as a named system rather than as the phrase non-toxic PVC.
- Material and construction: unsupported film or coated base fabric, named polymer, scrim if coated.
- Thickness: target in millimetres, tolerance band, equivalent grams per square metre at stated density.
- Optics: haze target and transmission target, with the measurement method named.
- Seams: joining method, seam width in millimetres, corner radius, required weld efficiency or peel value.
- Closure: zipper type and size in standard zipper terminology, tape material, end-stop termination.
- Branding: print method, ink system, artwork placement, maximum opaque coverage per face.
- Plasticiser system: named chemistry, phthalate-free statement, markets the restriction applies to.
- Appearance retention: stabiliser and UV package, yellowing expectation, odour grade after defined conditioning.
- Compatibility: contact test against the brand's actual formulations, with temperature, duration, criterion.
- Tests and evidence: which methods, which laboratory, per batch or per programme.
- Inspection: AQL level, sampling standard, defect classification list specific to clear film.
- Programme terms: minimum order quantity, sampling duration, bulk lead time, shipment and payment terms.
- Restricted-substance screening report — phthalate screening by GC-MS, covering all plasticised components including print and tape, not just the body film.
- REACH candidate-list statement — a declaration addressing substances of very high concern above the reporting threshold.
- Children's-product report where applicable — phthalate and heavy-metal migration limits under the applicable CPSIA or toy-safety method.
- Coated-fabric mechanical report — tensile, tear, coating adhesion and low-temperature bend under the ASTM D751 framework.
- Colour-fastness report — rubbing and perspiration fastness on any dyed textile component under the ISO 105 series.
- Seam performance evidence — peel or shear values and a documented leak or hold-out test on the finished construction.
- Bill of materials — film compound, plasticiser system, stabiliser, ink, tape, zipper and lining, each identified so the laboratory can test the real construction.
Two practical points make laboratory evidence useful rather than decorative. First, the tested sample must be the finished construction, including print, tape, zipper and lining, because a restriction applies to the article as sold and a clear film sample without its printed border can pass while the finished bag fails. Second, reports should be dated and tied to a batch or a formulation revision, because a compound change at the film mill invalidates an old report.
On the programme side, the commercial constants for a custom clear cosmetic bag are straightforward. Minimum order quantity is 500 pieces per style and colourway. Sampling runs 6-10 working days, extending to 12-15 working days for multi-panel welded or moulded constructions. Bulk production runs 35-50 days after sample approval. Inspection is at AQL 2.5 under the ISO 2859-1 sampling procedures, and the defect list for a clear film product should include haze, bloom, crease whitening, weld thinning and print adhesion, which no general-purpose bag checklist mentions. Shipment is on FOB Xiamen terms with payment structured as T/T 30 percent deposit and 70 percent against bill of lading. QUANZHOU JUNYUAN BAGS coordinates programmes of this kind as a sourcing and programme-management company, working with SGS-verified production floor space of 4,950 square metres across seven production lines and 149 machines, with monthly output capacity of 200,000 pieces.
The B2B Customisation View
The route from concept to shelf for makeup bags and toiletry bags is short when the specification is tight at the start, and painfully long when it is not.
Fixed commercial parameters: 500 pieces per style and colourway minimum, first sample in 6–10 working days (12–15 for complex or hardware-intensive constructions), bulk 35–50 days after approval, AQL 2.5 inspection under ISO 2859-1, FOB Xiamen, T/T 30/70.
The role played here is programme coordinator: QUANZHOU JUNYUAN BAGS translates a retail brief into a factory-ready technical pack and then audits the output against it before goods leave the floor.
Which Brand Types This Guide Serves
Transparent construction serves a wider spread of buyer types than most cosmetic bag formats, because the reasons for wanting it differ. A start-up skincare brand wants a clear pouch as a packaging statement and for airport-friendly travel kits. An established colour-cosmetics brand wants a gift-with-purchase that will not read as cheap. A retailer wants an own-brand travel accessory with a defensible compliance file. An e-commerce seller wants it because search demand is measurable, with toiletry bag searches running at roughly 74,810 per week on Amazon according to ASINSIGHT data for July 2026 and travel bag for toiletries at around 110,000 per month, both demand signals rather than revenue figures.
- Start-up and indie beauty brands — a clear pouch differentiates a first launch at low tooling cost, but the non-phthalate system must be specified from the first sample.
- Established colour cosmetics and skincare brands — transparent gift-with-purchase and travel kits, where odour and print adhesion generate the most complaints.
- Retailers and own-brand programmes — need a full restricted-substance file and a named plasticiser system, because the retailer carries the labelling risk.
- E-commerce and marketplace sellers — haze, crease whitening and odour on arrival directly affect returns.
- Travel and airline-adjacent buyers — quart-size toiletry bags driven by carry-on liquids rules; the bag must be genuinely transparent and close reliably.
- Event, festival and venue merchandise buyers — clear bags sold for entry compliance, where the buyer must verify each venue's current published policy and avoid printing unsubstantiated approval claims.
- Hospitality and amenity buyers — transparent amenity pouches for spas and hotels, where soft hand and low odour matter more than long-term clarity retention.
- Promotional and gift-with-purchase buyers — short-life pouches where heat-sealed lightweight film keeps unit cost in the low end of the typical $0.45-$12.00 marketplace band, treated as an illustrative planning range.
What these buyers share is that the failure modes are invisible in a photograph. Haze, blocking marks, crease whitening, cold cracking, bloom and odour cannot be judged from a single sample handled at room temperature on the day it arrives. Specifying film gauge, plasticiser system, seam method and laboratory evidence up front converts a category that generates returns into one that generates repeat orders.
Frequently Asked Questions
What gauge of PVC should a clear cosmetic bag be specified at, and why does it matter so much?
Gauge should be stated in millimetres with an equivalent weight in grams per square metre, because the two figures together prevent the mil-versus-gauge confusion that causes mismatched quotations. A flat zip pouch up to about 24 cm wide typically sits at 0.15 to 0.20 mm, a hanging toiletry kit at 0.20 to 0.25 mm, and a structured vanity case at 0.30 to 0.45 mm. Bending stiffness rises with the cube of thickness, so a small increase in gauge produces a dramatic change in hand, and thickness also sets the welding energy and dwell required.
Is PVC or TPU the better choice for a transparent toiletry bag sold into cold climates?
TPU is the safer choice for cold distribution because its flexibility comes from the polymer chain rather than from a plasticiser that loses solvating power as temperature falls, so it stays flexible well below freezing without any formulation gamble. Flexible PVC can perform acceptably in cold conditions, but only when a low-temperature plasticiser such as an adipate, sebacate or cycloaliphatic non-phthalate type is specified and verified by a low-temperature bend test. Buyers selling into markets with unheated warehousing should state the conditioning temperature and acceptance criterion rather than asking generically for cold resistance.
Why does a clear PVC pouch turn cloudy after a few weeks in a warehouse?
Clouding usually has one of three causes, and they look similar but have different fixes. Plasticiser bloom is the plasticiser migrating to the surface and scattering light, which points to a low-molecular-weight plasticiser system. Blocking is the film adhering to itself under heat and pressure in storage, leaving broad patches, which points to missing anti-block additive or cartoning while still warm. Inter-layer fogging is moisture trapped between stacked panels, which points to humid shipment conditions and airtight packing. Identifying which one is present determines whether the fix belongs in the compound, the cooling step or the carton.
Can a clear cosmetic bag be made genuinely liquid-tight for shampoo and oils?
Yes, when the perimeter seam is welded rather than sewn and the closure is terminated correctly. Radio-frequency welding fuses polar films such as PVC and TPU into a continuous seam, and a well-tuned weld can approach the strength of the parent film. The leak risk then moves to the zipper end stops, where an incompletely terminated weld leaves a capillary channel, and to the corner radii, where sharp geometry thins the seam. Buyers should require a documented leak or hold-out test on the finished construction rather than a visual check of the weld bead.
How much print coverage can a clear bag carry before it stops being see-through?
There is no fixed percentage in any standard, because the threshold depends on whether the bag is being sold for a screening purpose and on what the specific venue or operator permits. As an illustrative planning guide, many programmes keep opaque coverage below roughly a quarter of each face and place artwork in a header band, a border frame or a corner block so the central window remains unobstructed. For compliance-sensitive styles, a woven label in the binding or a logo plate on the puller carries the brand with almost no loss of viewing area.
Does a clear bag have to be transparent on every panel to be accepted at a venue gate?
Requirements are set by each venue operator and differ between venues that look similar, and they are revised between seasons, so there is no universal rule to design against. Some operators require the entire bag to be transparent, some permit a small opaque clutch or a printed border, and some prohibit bags of any kind. A buyer supplying bags for venue entry must verify the requirement against the specific venue's current published policy in writing before committing to artwork and tooling, and should not treat any stated dimension as an industry standard.
Which plasticisers should be ruled out when a clear PVC bag is sold into the EU or the US?
Several ortho-phthalates, including DEHP, DBP, BBP and DIBP, are restricted in articles in the EU above a low percentage threshold of the plasticised material under the REACH framework administered by the European Chemicals Agency, so a European-bound programme is normally specified as non-phthalate from the outset. In the US, the Consumer Product Safety Improvement Act sets phthalate limits for children's products and child care articles, and California maintains a separate listed-substance regime. The specification should name the destination markets and the plasticiser system rather than relying on the phrase non-toxic PVC.
How strong is a welded seam compared with the film around it, and how is that measured?
Seam quality is expressed as weld efficiency, the joint strength as a percentage of the parent film strength, and a well-tuned radio-frequency weld on PVC can approach the parent material so that the film tears before the seam separates. Measurement is by shear testing, pulling the seam in line, and by peel testing, separating it, and for coated fabrics the conventional framework for tensile, tear and adhesion measurement is ASTM D751. Buyers should also request a hydrostatic or hold-out result appropriate to the construction, because a strong seam that weeps is still a failed seam.
How should odour on a new PVC pouch be assessed before a bulk order ships?
Odour comes from residual solvent, residual monomer and the volatile fraction of the plasticiser, and it fades with time but not reliably before the customer opens the bag. The practical controls are low-odour plasticiser and ink systems, a defined aeration period between production and packing, and avoiding sealing a warm bag inside an airtight polybag. Assessment should be a graded panel evaluation under stated conditioning, with a maximum grade written into the specification, and an odour grading scale adapted from an adjacent industry such as automotive interiors can serve as an internal acceptance method.
Will sunscreen, alcohol or nail polish remover damage the inside of a clear PVC bag?
Potentially yes. Fragrance and essential oils, high-alcohol toners, acetone and some sunscreen filters extract plasticiser from PVC, softening, hazing or crazing the interior within a short period, and the damage appears on the bag floor where bottles stand. TPU resists oils and abrasion far better and is the usual upgrade path for oil-based product lines, while polyethylene-based films resist many solvents but bring clarity and stiffness compromises. A compatibility test should run the brand's actual formulation on the interior surface at a stated temperature and duration, with the acceptance criterion agreed before testing.
What is the difference between unsupported PVC film and PVC-coated polyester fabric?
Unsupported film is a single homogeneous sheet, which gives the cleanest weld and a fully uninterrupted window but no reinforcement, so a small nick can propagate across a panel. Coated fabric carries a woven polyester scrim inside the sheet, which arrests tears and lets the bag take handles, hooks and heavier loads, at the cost of slightly lower light transmission, visible weave texture, and cut edges that must be bound because the exposed scrim wicks water. Bags above roughly 30 cm in any dimension, or with any strap or hook, generally justify coated construction.
How does a buyer verify that a phthalate-free or non-toxic claim on a clear bag is real?
The claim has to be tied to a laboratory report on the finished article, not to the film alone. The tested sample must include print, seam tape, zipper and lining, because a restriction applies to the article as sold and a clear film sample without its printed border can pass while the finished bag fails. Buyers should request phthalate screening by gas chromatography-mass spectrometry, a statement addressing substances of very high concern, and reports that are dated and tied to a batch or formulation revision, since a compound change at the film mill invalidates an old certificate.
Do clear PVC bags yellow over time, and can yellowing be slowed?
Yellowing is real and has two mechanisms with different fixes. In PVC, heat or UV exposure strips hydrogen chloride from the chain, creating conjugated bonds that absorb visible light and turn the film yellow then brown; a modern calcium-zinc stabiliser package with a co-stabiliser is the defence. In TPU, yellowing is usually photo-oxidation of aromatic segments, addressed by an aliphatic grade or by UV absorbers and light stabilisers. Storage matters too, because nitrogen oxides reacting with phenolic antioxidants in cartons can transfer discoloration, so packaging choice belongs in the specification.
What laboratory evidence should be requested before approving a clear PVC bag programme?
A complete file normally includes restricted-substance screening covering every plasticised component, a declaration addressing substances of very high concern, children's-product reports where the market or positioning requires them, coated-fabric mechanical results covering tensile, tear, adhesion and low-temperature bend, colour-fastness results for any dyed textile component, and documented seam peel or leak evidence on the finished construction. A full bill of materials should accompany the samples so the laboratory tests the real article. Reports should be dated, tied to a formulation revision, and treated as a living file rather than a one-time certificate.
People Also Ask
Are clear cosmetic bags allowed in stadiums?
Entry rules are set by each venue operator, not by any industry standard, and they are revised between seasons, so a dimension that was accepted last year may not be accepted now. Some venues require fully transparent bags, some allow a small opaque clutch, and some prohibit bags entirely. Buyers supplying bags for venue entry should verify the requirement against the specific venue's current published policy in writing and should avoid printing unsubstantiated approval claims on the product.
Why do clear makeup bags smell like a shower curtain?
The smell comes from volatile compounds leaving flexible PVC: residual solvent from printing, residual monomer, and the more volatile fraction of the plasticiser. It fades over time but not reliably before the customer opens the carton. Specifying low-odour plasticiser and ink systems, requiring an aeration period before packing, and avoiding airtight packing while the bag is still warm all reduce it, and a graded odour acceptance limit makes the expectation enforceable.
What is the difference between PVC and TPU cosmetic bags?
Flexible PVC is resin compounded with a plasticiser, so its softness comes from a liquid that can migrate, evaporate, be extracted by oils, or fall under chemical restriction. TPU is an elastomer that needs no plasticiser, giving better cold flex, better oil and abrasion resistance and lower odour at a material cost several times higher. PVC welds superbly under radio-frequency energy and costs less; TPU is chosen for premium, cold-climate and oil-heavy programmes.
How thick should a clear toiletry bag be?
Thickness depends on the format. A flat zip pouch sits around 0.15 to 0.20 mm, a hanging kit with compartments around 0.20 to 0.25 mm, and a structured vanity case around 0.30 to 0.45 mm. Because bending stiffness rises with the cube of thickness, a modest increase makes the bag dramatically stiffer, so buyers wanting structure are often better served by a thinner coated fabric with binding than by simply ordering thicker film.
Do clear PVC bags turn yellow?
They can. Heat and UV exposure can strip hydrogen chloride from the PVC chain and create light-absorbing bonds that turn the film yellow then brown, which is controlled by the heat stabiliser package. Aromatic TPU yellows by a different route, photo-oxidation, and is addressed with an aliphatic grade or UV absorbers. Storage conditions contribute as well, since nitrogen oxides reacting with antioxidants in cartons can transfer discoloration to the bag.
References & Standards
- ISO 2859-1 sampling procedures for inspection by attributes
- ASTM D2053 standard terminology relating to zippers
- AATCC TM61 colour fastness to laundering
- IEC 62321 determination of certain substances in electrotechnical products
- OEKO-TEX Standard 100 testing for harmful substances
- Textile Exchange Global Recycled Standard
- US CPSC CPSIA consumer product safety improvement act
- ECHA REACH regulation on chemicals
- TSA 3-1-1 liquids rule for carry-on baggage
- ASTM D751 standard test methods for coated fabrics
- ISO 105 textiles tests for colour fastness
- Global Organic Textile Standard GOTS
In-Depth Articles in This Category
14 dedicated articles sit under this pillar guide.
Related Pillar Guides
Request a Sample or a Written Quotation
Send the silhouette, dimensions, material preference and logo artwork, and the programme team will return a written quotation with MOQ, sampling window, bulk lead time and inspection standard.
Email: service@junyuanbags.com · WhatsApp: +86 177 5002 0688